Duo-Finish RTA Kitchen in Flint Grey and Porcini, Twelve Units Flat-Packed
One carcass SKU and one door carton: 1.04 m3 for twelve units, about 65 packs to a 40HQ, and a finish change that costs a carton rather than a program
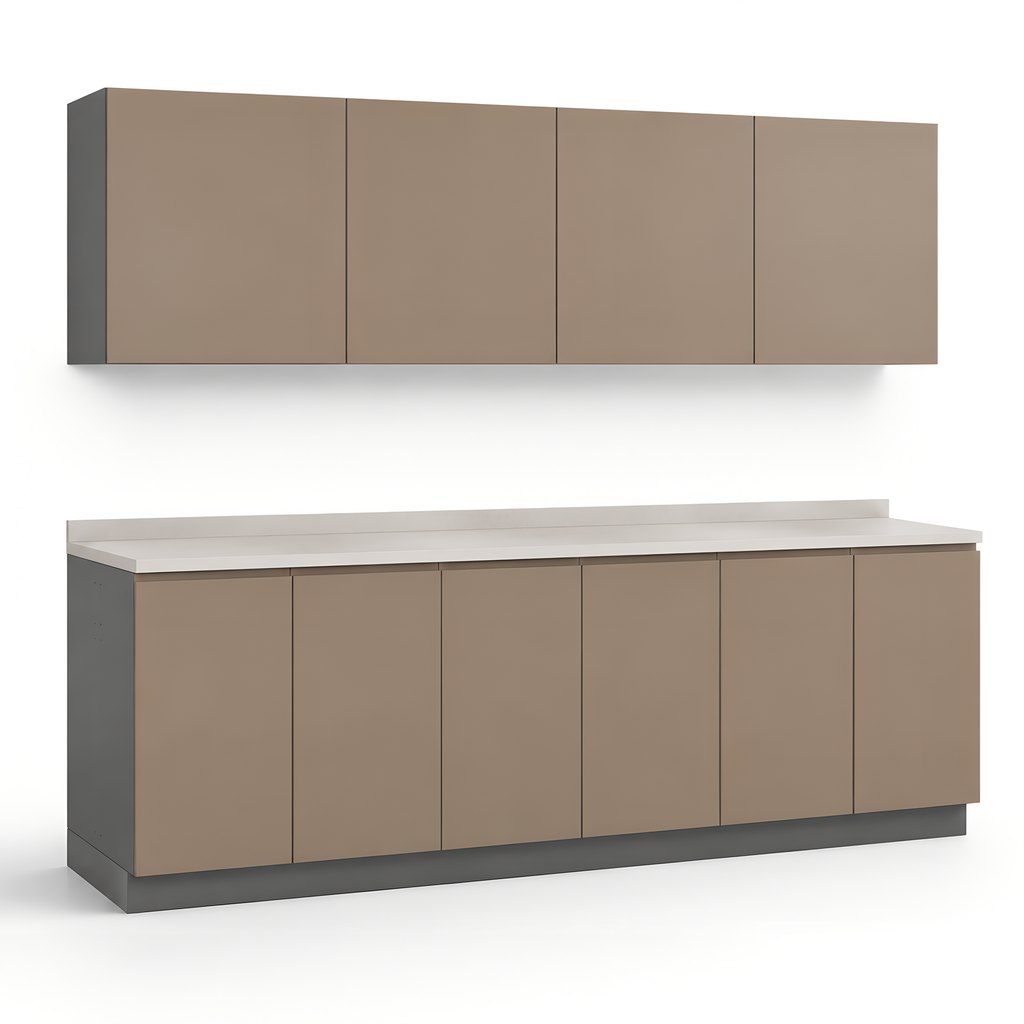
A kitchen in two finishes is normally two spray batches, two foil runs and two programs to hold in stock. This pack separates the two at the carton line: every carcass ships in flint grey melamine, complete and drilled, and the door fronts ship in their own carton in porcini super-matte. A dealer stocks one carcass and swaps the front carton, which is the difference between carrying a trend and committing to it. Twelve units on Australian geometry, 720 x 560 mm base and 720 x 350 mm wall, 18 mm EN 312 P3 board in E1 with 32 mm system drilling. Fifteen cartons at 1.04 m3 and 138 kg, about 65 packs to a 40HQ.
- ModelFAME-KC-MFC-DF
- Module set6 base at 600+600+600+500+300+400 mm = 3,000 mm; 4 wall at 600+600+500+300 mm = 2,000 mm; 2 tall (600 mm oven tower, 500 mm larder); 12 units total
- Base unit720 mm high x 560 mm deep, 18 mm EN 312 P3 board in E1, 5 mm HDF back, 4 adjustable legs, flint grey melamine inside and out
- Wall unit720 mm high x 350 mm deep, two adjustable shelves on 4 mm pins at 32 mm pitch, flint grey melamine interior
- Tall unit2,010 mm high x 560 mm deep; 600 mm oven tower with a 600 mm appliance void and a fixed mid shelf, 500 mm larder with four shelves
- Doors and fronts18 mm MFC slab, porcini super-matte, 4 to 6 gloss units, 1 mm ABS laser edge, 3 mm reveal, packed as a separate carton so the carcass can ship in any finish
Trade inquiry only — this is a B2B catalog with no online checkout. Our team replies within 24 hours.
Full Specification
- ModelFAME-KC-MFC-DF
- Module set6 base at 600+600+600+500+300+400 mm = 3,000 mm; 4 wall at 600+600+500+300 mm = 2,000 mm; 2 tall (600 mm oven tower, 500 mm larder); 12 units total
- Base unit720 mm high x 560 mm deep, 18 mm EN 312 P3 board in E1, 5 mm HDF back, 4 adjustable legs, flint grey melamine inside and out
- Wall unit720 mm high x 350 mm deep, two adjustable shelves on 4 mm pins at 32 mm pitch, flint grey melamine interior
- Tall unit2,010 mm high x 560 mm deep; 600 mm oven tower with a 600 mm appliance void and a fixed mid shelf, 500 mm larder with four shelves
- Doors and fronts18 mm MFC slab, porcini super-matte, 4 to 6 gloss units, 1 mm ABS laser edge, 3 mm reveal, packed as a separate carton so the carcass can ship in any finish
- Hinges and drawersDTC 110 degree clip-on hinges, 3D cam, 40,000 cycles; DTC 30 kg tandem drawers, soft close, 50,000 cycles on a 16 mm base panel; two of the 600 mm bases carry a three-drawer bank
- Plinth and worktop150 mm adjustable plinth with 4 legs per unit and 2,400 mm of clip-on kick board in flint grey; worktop not included, 33 mm laminate or 20 mm stone quoted against the module list
- Bench height720 mm carcass + 150 mm plinth + 33 mm laminate = 903 mm; on a 20 mm stone top the same carcass lands at 890 mm, so the top has to be fixed before the legs are set
- Packing15 cartons, 1.04 m3, 138 kg gross per pack: 6 base, 4 wall, 2 tall, 1 fronts, 1 hardware, 1 plinth
- Carton sizeLargest carton 2,050 x 590 x 95 mm (tall panels, floor-loaded); the other fourteen fit a 1,200 x 800 pallet
- Loading quantityAbout 65 packs per 40HQ at 68 m3 usable, about 27 packs per 20GP
- MOQ20 sets per finish, with the carcass and the door finish counted separately
- Lead time25-30 days after deposit and cutting list confirmation
- Loading portNingbo / Shanghai, FOB
Why Buyers Choose This Model
- Twelve units from one cutting list: six base at 600+600+600+500+300+400 mm (3,000 mm of run), four wall at 600+600+500+300 mm (2,000 mm), plus a 600 mm oven tower and a 500 mm larder, both 2,010 mm high
- One carcass SKU in flint grey melamine inside and out across all 12 units, so a second finish is one carton of 12 fronts rather than a second program, a second minimum and a second set of drawings
- Doors travel in their own carton: 18 mm MFC slab, porcini super-matte at 4 to 6 gloss units, 1 mm ABS laser edge on four sides, so a front damaged in year three is a carton from stock, not a spray batch to color-match
- 18 mm EN 312 P3 board in E1 emission class with a 5 mm HDF back and 32 mm system drilling on every side panel, so a shelf moves on 32 mm pitch without a new panel and a slow leak does not open a seam
- 720 mm base carcass on a 150 mm adjustable plinth under a 33 mm laminate top lands the bench at 903 mm, which is the number an Australian fitter sets the legs to rather than a nominal 900 read off a plan
- 560 mm base depth and an 18 mm door put the door face at 578 mm under a 600 mm benchtop, leaving 22 mm of overhang, which is the clearance that keeps a spill on the bench and off the door
- DTC 110 degree clip-on hinges at 40,000 cycles and DTC 30 kg tandem drawers at 50,000 cycles, with one hardware bag per carton and a numbered panel set, so a fitter is not sorting a mixed bag on site
- Fifteen cartons at 1.04 m3 and 138 kg gross, about 65 packs per 40HQ; the 2,050 mm tall-panel carton is floor-loaded and the other fourteen fit a 1,200 x 800 pallet
Specification Questions Buyers Ask
Why split the carcass and the door finish instead of making one finished kitchen?
Does 560 mm of carcass depth leave enough overhang on an Australian benchtop?
Is 903 mm the bench height I should specify?
Can the widths inside the twelve units change inside the minimum?
How do I turn the twelve-unit list into a container plan?
Building a Kitchen Cabinets Program?
Send your target market, sizes and quantities — we reply within 24 hours with a tailored quotation.